
VFD for wire-cut EDM
I. Overview
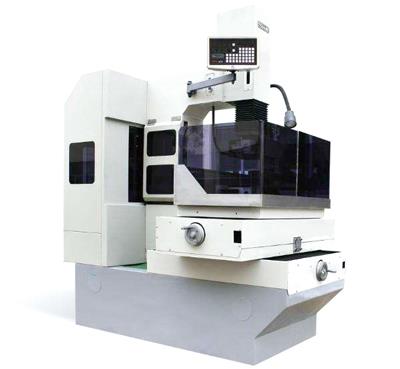
The wire-cut EDM is to utilize the metal linear tool electrode (or named as wire electrode) to process workpieces with the principle of impulsive discharge to erode the metals. High speed wire-cut EDM is applied in the processing of the metal pieces with high precision, complicated shape, especially the mould and so on.
II. The contrast before and after using the VFD
The electrical and motor control parts of the wire-cut EDM. The wire bucket motor control part controls the motor and the wire bucket, drives the molybdenum wire to have fast negative and positive starting operation and stopping. In addition, it will provide the corresponding protective functions. The electrical control of other types of the machinery tools usually employs the relay control mode, which is also practical. However, such control mean has the following a series of problems:
- The contactor of the relay has frequent movement and relatively high consumption. The intermediate conversion is complicated and the possibility of having problems is high.
- The frequent positive and negative full-pressure starting of the motor has big starting current and big shock to the mechanical part of the wire bucket.
- The frequent close and disconnection of the touch spot of the contactor, thus causing great noise.
The main consequence resulted by such problems is the declining of the entire processing reliability, increasing of the wire burning and other problems. Therefore, it is sure to generate a second processing, thus affecting the product quality and generating unnecessary economic loss finally. Aimed at the above existing problems, the VFD with small power has been used to improve the original control mode. The reason mainly includes the following several points:
- The frequency conversion products have matured technology and reliable performance. They have been widely used in the control systems of the induction motor widely.
- Utilizing the circumscribed control input terminal, output terminal which reflects the operating status and the powerful programmable function of the VFD, flexible selections and settings can be conducted according to the different control objects and control means, thus saving the complicated switching control in the middle.
- The starting and stopping time as well as the current of the motor can be completed through manual coding and automatic setting, which has reduced the disadvantages of the original mean with big starting current and mechanical shock.
- The phase sequence switch of the main circuit is completed through the internal integrated control circuit in the VFD (no touch point switchover). In addition, there is also DC braking function in the VFD. And it has been set that when the revolving speed of the motor becomes 0, the braking process can be eliminated automatically, thus avoiding the unnecessary big current sustained by the motor caused by improper operation.
III. The parameter setting of ATO VFD is as follows:
| Function code | Name | Setting range | Set value |
| P0.02 | Unilateral cutting reverse speed | P0.19 lower limiting frequency~P0.20 upper limiting frequency | 50.00Hz |
| P3.00 | Mean of the processing finishes | 0: Immediate deceleration + DC braking stop 1: Left entering of positive revolving signal valid stop 2: Right entering of negative revolving signal valid stop | 0 |
| P3.02 | Operating mode | 0: Switch inverting, 1: Timely inverting, 2: Unilateral cutting | 0 |
| P3.03 | Effective polarity of processing finishes | 0: Normal open, 1: Normal closed | 1 |
| P3.11 | Reversing delay time | 0s~5.0s | 0.1 |
| P0.17 | Acceleration time 1 | 0.1~6000.0 | 0.5 |
| P0.18 | Deceleration time 1 | 0.1~6000.0 | 0.5 |
| P3.14 | Acceleration time 2 | 0.1~6000.0 | 0.5 |
| P3.15 | Deceleration time 2 | 0.1~6000.0 | 0.5 |
| P3.16 | Acceleration time 3 | 0.1~6000.0 | 0.5 |
| P3.17 | Deceleration time 3 | 0.1~6000.0 | 0.5 |
| P3.18 | Acceleration time 4 | 0.1~6000.0 | 0.5 |
| P3.19 | Deceleration time 4 | 0.1~6000.0 | 0.5 |
| P3.20 | Acceleration time 5 | 0.1~6000.0 | 0.5 |
| P3.21 | Deceleration time 5 | 0.1~6000.0 | 0.5 |
| P3.22 | Acceleration time 6 | 0.1~6000.0 | 0.5 |
| P3.23 | Deceleration time 6 | 0.1~6000.0 | 0.5 |
| P3.24 | Acceleration time 7 | 0.1~6000.0 | 0.5 |
| P3.25 | Deceleration time 7 | 0.1~6000.0 | 0.5 |
| P3.26 | Multistage frequency 1 | P0.19 lower limiting frequency~P0.20 upper limiting frequency | 50.00Hz |
| P3.27 | Multistage frequency 2 | P0.19 lower limiting frequency~P0.20 upper limiting frequency | 40.00Hz |
| P3.28 | Multistage frequency 3 | P0.19 lower limiting frequency~P0.20 upper limiting frequency | 30.00Hz |
| P3.29 | Multistage frequency 4 | P0.19 lower limiting frequency~P0.20 upper limiting frequency | 25.00Hz |
| P3.30 | Multistage frequency 5 | P0.19 lower limiting frequency~P0.20 upper limiting frequency | 20.00Hz |
| P3.31 | Multistage frequency 6 | P0.19 lower limiting frequency~P0.20 upper limiting frequency | 15.00Hz |
| P3.32 | Multistage frequency 7 | P0.19 lower limiting frequency~P0.20 upper limiting frequency | 10.00Hz |
| P3.33 | Keyboard setting speed 1 | P0.19 lower limiting frequency~P0.20 upper limiting frequency | 5.00Hz |
| P3.34 | Keyboard setting speed 2 | P0.19 lower limiting frequency~P0.20 upper limiting frequency | 10.00Hz |
| P3.35 | Keyboard setting speed 3 | P0.19 lower limiting frequency~P0.20 upper limiting frequency | 20.00Hz |
| P3.36 | Keyboard speed set value | 1: P3.33, 2: P3.34, 3: P3.35 | 1 |
| P4.05 | Multistage speed control terminal 1 | 10.00Hz | |
| P4.06 | Multistage speed control terminal 2 | 20.00Hz | |
| P4.07 | Multistage speed control terminal 3 | 30.00Hz | |
| P8.00 | Simple PLC operating mode | 0113 | |
| P8.01 | Stage 1 setting | 000 | |
| P8.02 | Stage 1 time setting | 3 | |
| P8.03 | Stage 2 setting | 010 | |
| P8.04 | Stage 2 time setting | 5 | |
| P8.06 | Stage 3 time setting | 3 | |
| P8.08 | Stage 4 time setting | 5 | |
| P8.10 | Stage 5 time setting | 0 | |
| P8.12 | Stage 6 time setting | 0 | |
| P8.14 | Stage 7 time setting | 0 |
Buying an ATO VFD for wire-cut EDM speed control now, 2 hp VFD, 3 hp VFD, 5 hp VFD...