
Servo Spindle Motors
Quick Answer: What is an AC Servo Spindle Motor?
An AC servo spindle motor is a CNC machine spindle drive that combines continuous high-speed rotation with closed-loop encoder feedback for precision machining. It operates as an asynchronous vector drive capable of instant switching between speed regulation and angular positioning.
- Core Components: 3-phase asynchronous motor body, integrated high-speed photoelectric encoder.
- Control Architecture: Dual-mode vector control (Velocity Mode / Position Mode).
- Primary Compatibility: CNC milling machines, vertical machining centers (VMC), and CNC lathes.
If-Then Decision Matrix: Servo Spindle Motors Power Class Selection
| If Machining Requirement Is | Then Choose Power Class | Voltage Supply: | Recommended ATO SKU: |
Standard CNC Milling
| Low-to-Medium Power 2.2 kW – 5.5 kW (3 hp – 7.5 hp) | 3-Phase 220V / 380V | ATO-SERVO-314 (2.2kW) |
| ATO-SERVO-524 (3.7kW) | |||
| ATO-SERVO-5535 (5.5kW) | |||
Heavy-Duty Cutting
| High-Torque Heavy-Duty 7.5 kW – 15 kW (10 hp – 20 hp) | 3-Phase 380V (7.5kW supports 220V/380V) | ATO-SERVO-1050 (7.5kW) |
| ATO-SERVO-9560 (9.5kW) | |||
| ATO-SERVO-1170 (11kW) | |||
| ATO-SERVO-2095 (15kW) |
Servo Spindle Motor Technical Summary
Spindle Motor vs. Servo Spindle Motor
- Standard Spindle Motor: An open-loop CNC drive built exclusively for high-speed cutting without angular feedback.
- Servo Spindle Motor: A closed-loop CNC drive with encoder feedback supporting both cutting and position control.
Velocity Mode vs. Position Mode
- Velocity Mode: A vector speed control mode regulating continuous spindle rotation for uniform surface finishes.
- Position Mode: A closed-loop feedback mode utilizing encoder pulses for machine tool synchronization.
Core CNC Mechanics & Closed-Loop Functions
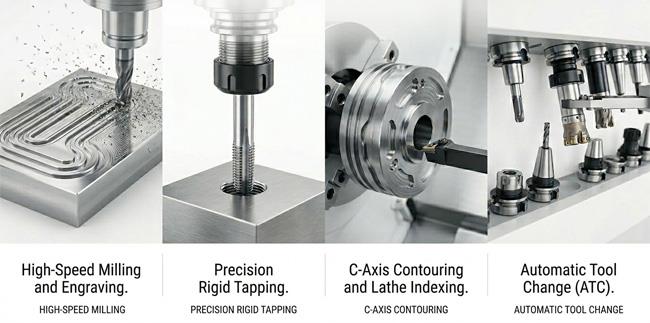
- Rigid Tapping: A synchronized machining process coordinating spindle rotation with Z-axis feeds for thread cutting.
- Zero-Speed Locking: A stationary holding function providing full rated torque at zero rpm for spindle braking.
- C-Axis Contouring: A multi-axis interpolation method enabling continuous workpiece indexing on automated turning centers.
Servo Spindle Motor Applications
ATO AC servo spindle motors improve machining efficiency in CNC automation across vertical machining centers (VMC) and complex lathe turning centers.
FAQs about Servo Spindle Motors
Q: What are Servo Spindle Motors used for?
A: Servo spindle motors drive CNC machine spindles for milling, turning, drilling, and engraving. They provide high-speed rotation with closed-loop position control for precision machining in CNC systems such as VMCs and lathes.
Q: What is velocity vs position mode?
A: Velocity mode controls spindle speed for machining operations like milling and engraving. Position mode controls spindle orientation for automatic tool change (ATC) and precise angular positioning.
Q: What is rigid tapping in CNC?
A: Rigid tapping is a synchronized machining process where spindle rotation is matched with Z-axis feed using encoder feedback. This ensures accurate thread pitch and prevents timing or synchronization errors.
Q: How to choose a servo spindle motor?
A: Selection depends on power and machining load. 2.2–5.5 kW models are used for light CNC milling and tapping, while 7.5–15 kW models are used for heavy cutting, CNC lathes, and high-torque applications.

3 hp (2.2 kW) AC Servo Spindle Motor, 14 Nm, 1460 rpm

5 hp (3.7 kW) AC Servo Spindle Motor, 24 Nm, 1460 rpm

5.5 kW AC Servo Spindle Motor, 35 Nm, 1460 rpm

10 hp (7.5 kW) AC Servo Spindle Motor, 50 Nm, 1460 rpm

9.5 kW AC Servo Spindle Motor, 60 Nm, 1500 rpm

11 kW AC Servo Spindle Motor, 70 Nm, 1500 rpm


