Infrared Temperature Sensor, Non-Contact, 0 ~ 1200℃

$439.79
Low price non-contact infrared temperature sensor online sale, with 4-20mA or RS485 signal output, object distance ratio 20:1, accuracy ±2% or ±2℃, easy assembly and high precision. This industrial IR temperature sensor with infrared measurement, can measure 0 ~ 1200℃ temperature.
SKU: ATO-IR-400A
*
*
*
Free Shipping
Delivery date: 6-12 days

Industrial non-contact infrared temperature sensor with high performance sensor probe can detect reflect light. IR temperature sensor can measure temperature continuously, millisecond response speed, small in size, suitable for narrow working conditions.

Specification

ModelATO-BRW600-400A
Measurement Range0 ~ 100℃, 200℃, 300℃, 400℃, 500℃, 600℃, 700℃, 800℃, 900℃, 1000℃, 1200℃ (Optional)
Object Distance Ratio20:01
Power Supply10 ~ 30VDC / 5 ~ 30VDC
Accuracy±2% or ±2℃
Emissivity0.95
Signal Output4–20 mA or RS485 (Optional)
Working Temperature85℃
Response Time200 ms
Response Wavelength8 – 14 μm
Maximum Current< 50 mA
Storage Temperature-40 ~ 85℃
Ambient Temperature0 ~ 60℃ (Better performance at 0 ~ 50℃)
Relative Humidity10 ~ 95% RH (No condensation)
Protection GradeIP65
DimensionL119mm × φ18.7mm
Shell MaterialStainless Steel
Weight1 kg


Feature

  • Silicon-Based Microtechnology: Non-contact infrared temperature sensor has a highly sensitive temperature coefficient and excellent infrared detection for accurate and natural temperature measurement.
  • High-Speed Processing Chip: Built-in high-performance processor ensures rapid signal conversion for more stable and precise data output.
  • Strong Anti-Interference: Designed with robust EMI resistance, allowing stable operation even in complex electromagnetic environments.
  • Stainless Steel Housing: Made from premium 304 stainless steel, offering excellent corrosion resistance and durability in high-temperature environments.

Dimension (Unit: mm)
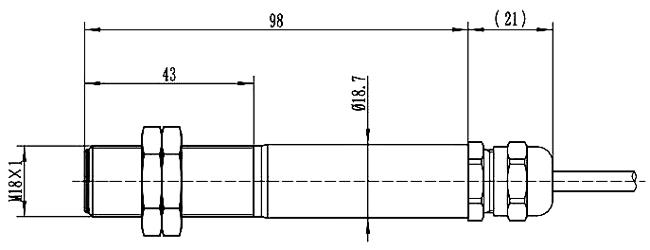
Dimensions of non-contact infrared temperature sensor

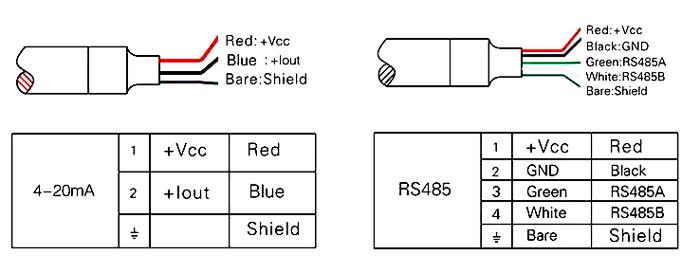
Wiring

Wiring of infrared temperature sensor

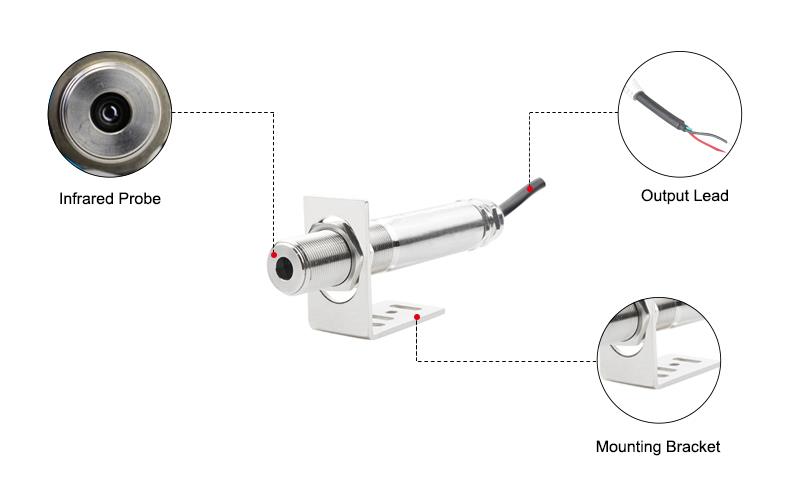
Detail

Infrared Temperature Sensor Details

Application

Applied in power equipment, medical field, process and production industries, metallurgy, petrochemical, electric power, light industry, textile industry, food industry, national defense, and scientific research fields.
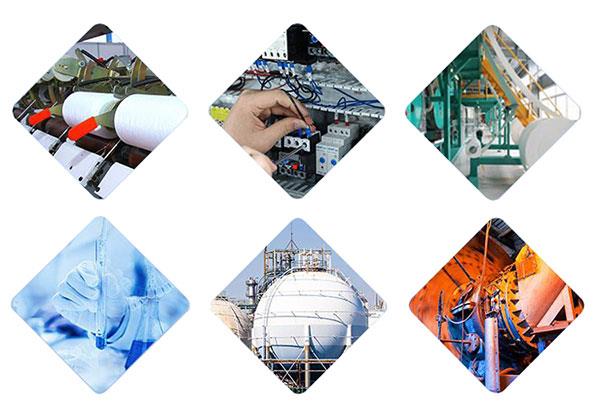
Infrared temperature sensor non contact application

Tips: Infrared temperature sensor for electrical power system

Many equipment accidents in the power system are initially caused by abnormal heating, and many substations with a large number of electrical equipment have implemented unattended working conditions. If these equipment are under high load for a long time, the temperature will often rise, which is often invisible to the human eye at first, eventually leading to thermal failure when the temperature increases cumulatively.

The use of infrared temperature sensors to monitor the temperature of electrical equipment in operation can directly observe whether there is a suspected fault in the equipment. By combining with the Internet of Things, cloud computing, and other technologies, the monitored equipment temperature and other abnormal events can effectively help power workers solve thermal faults and defects in the operation of substation equipment, and ensure the healthy operation of electrical equipment.

In this video, ATO will show you top ten most used sensors (sensing technologies).

Product reviews
Fast response and reliable output
5
Victoria
Avatar
8/25/2026 7:07 PM
The main reason we selected this sensor was the fast response and non-contact measurement. It works well with our PLC system through the analog signal output. The temperature data is stable, and commissioning was easier than expected.
Was this review helpful? Yes No (0/0)
Write your review
  • Only registered users can write reviews
*
*
  • Bad
  • Excellent
*
*
*
*

Industrial non-contact infrared temperature sensor with high performance sensor probe can detect reflect light. IR temperature sensor can measure temperature continuously, millisecond response speed, small in size, suitable for narrow working conditions.

Specification

ModelATO-BRW600-400A
Measurement Range0 ~ 100℃, 200℃, 300℃, 400℃, 500℃, 600℃, 700℃, 800℃, 900℃, 1000℃, 1200℃ (Optional)
Object Distance Ratio20:01
Power Supply10 ~ 30VDC / 5 ~ 30VDC
Accuracy±2% or ±2℃
Emissivity0.95
Signal Output4–20 mA or RS485 (Optional)
Working Temperature85℃
Response Time200 ms
Response Wavelength8 – 14 μm
Maximum Current< 50 mA
Storage Temperature-40 ~ 85℃
Ambient Temperature0 ~ 60℃ (Better performance at 0 ~ 50℃)
Relative Humidity10 ~ 95% RH (No condensation)
Protection GradeIP65
DimensionL119mm × φ18.7mm
Shell MaterialStainless Steel
Weight1 kg


Feature

  • Silicon-Based Microtechnology: Non-contact infrared temperature sensor has a highly sensitive temperature coefficient and excellent infrared detection for accurate and natural temperature measurement.
  • High-Speed Processing Chip: Built-in high-performance processor ensures rapid signal conversion for more stable and precise data output.
  • Strong Anti-Interference: Designed with robust EMI resistance, allowing stable operation even in complex electromagnetic environments.
  • Stainless Steel Housing: Made from premium 304 stainless steel, offering excellent corrosion resistance and durability in high-temperature environments.

Dimension (Unit: mm)

Dimensions of non-contact infrared temperature sensor

Wiring

Wiring of infrared temperature sensor

Detail

Infrared Temperature Sensor Details

Application

Applied in power equipment, medical field, process and production industries, metallurgy, petrochemical, electric power, light industry, textile industry, food industry, national defense, and scientific research fields.

Infrared temperature sensor non contact application

Tips: Infrared temperature sensor for electrical power system

Many equipment accidents in the power system are initially caused by abnormal heating, and many substations with a large number of electrical equipment have implemented unattended working conditions. If these equipment are under high load for a long time, the temperature will often rise, which is often invisible to the human eye at first, eventually leading to thermal failure when the temperature increases cumulatively.

The use of infrared temperature sensors to monitor the temperature of electrical equipment in operation can directly observe whether there is a suspected fault in the equipment. By combining with the Internet of Things, cloud computing, and other technologies, the monitored equipment temperature and other abnormal events can effectively help power workers solve thermal faults and defects in the operation of substation equipment, and ensure the healthy operation of electrical equipment.

Product reviews
Fast response and reliable output
5
Victoria
Avatar
8/25/2026 7:07 PM
The main reason we selected this sensor was the fast response and non-contact measurement. It works well with our PLC system through the analog signal output. The temperature data is stable, and commissioning was easier than expected.
Was this review helpful? Yes No (0/0)
Only registered users can write reviews