
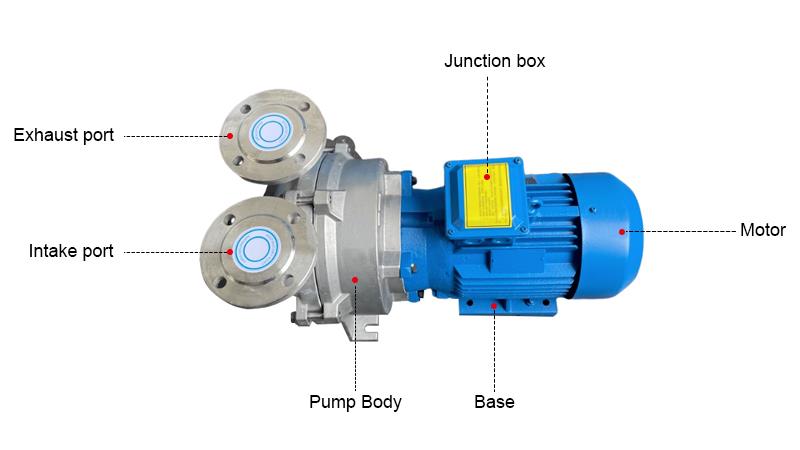
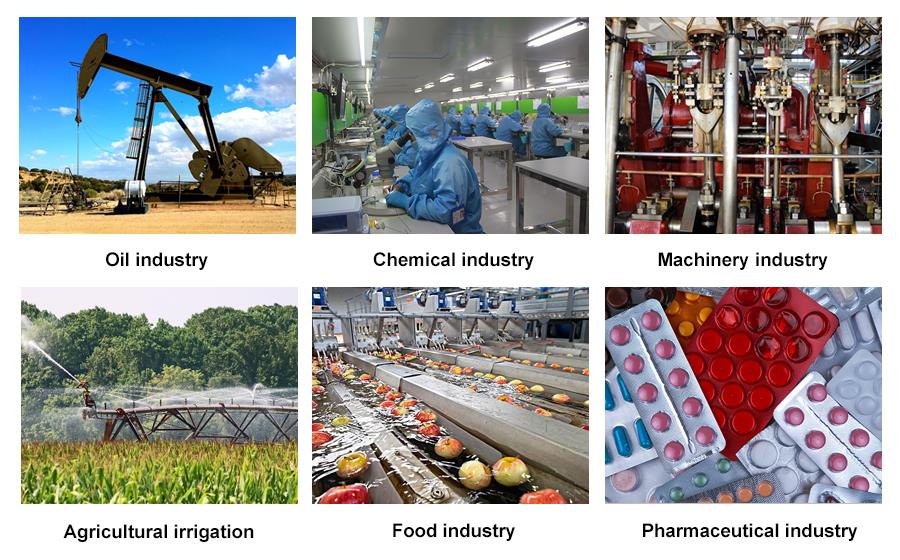
The unique design of the discharge port can protect the vacuun pump from the over-pressure to ensure the best efficient performance in the working range of the pump. 10 hp water ring pump often used in a variety of industries including chemical processing, food and beverage, pharmaceuticals, and more, where they play a critical role in processes such as vacuum filtration, distillation, drying, and degassing.
Features:
- Equipped with cavitation protection pipe interface.
- Flexible exhaust port design, no over compression.
- Designed with coaxial direct connection, which saves space and is easy to install.
- Vacuum pump adopts high quality mechanical seal as standard configuration.
Specification:
- Model: ATO-2BV5121
- Power: 10 hp (7.5 kW)
- Rated Voltage: 380V
- Phase: 3 phase
- Frequency: 50 Hz
- Max Gas Volume: 280 m3/h
- Extreme Pressure: 3300 Pa
- Noise: 69 dB
- Material: stainless steel
- Net Weight: 136kg
Details:
Dimension (Unit: mm)
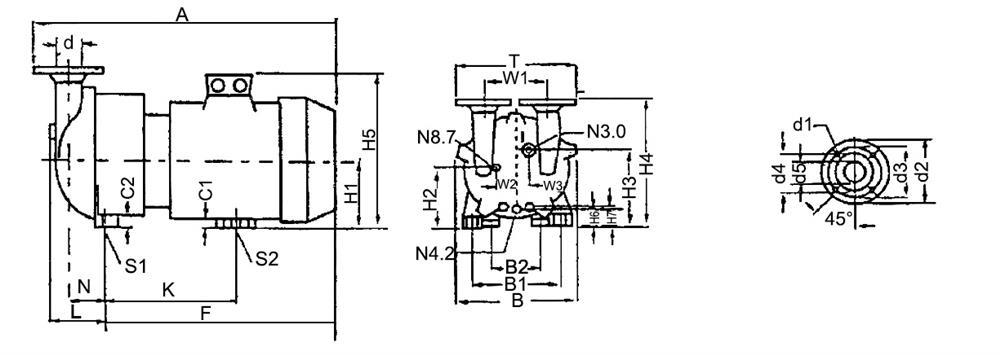
| 2BV5-121 | A | B | B1 | B2 | C1 | C2 | H1 |
| 771 | 347 | 265 | 216 | 36 | 26 | 150 | |
| H2 | H3 | H4 | H5 | H6 | H7 | K | |
| 165 | 217 | 385 | 363 | 39 | 62 | 425 | |
| L | F | N | S1 | S2 | T | d1 | |
| 147 | 584 | 105 | φ12×23 | φ12 | 382 | 19 | |
| d2 | d3 | d4 | d5 | W1 | W2 | W3 | |
| 182 | 145 | 113 | 66.5 | 200 | 57 | 29 | |
| N3.0 | N4.2 | N8.7 | / | / | / | / | |
| G3/4" | G3/8" | G3/8" | / | / | / | / |
Application:
Tips: Water Ring Vacuum Pump Disadvantages
- Water consumption. Water ring vacuum pumps require a continuous supply of water to create the sealing liquid ring that forms the vacuum. This can result in significant water consumption.
- Environmental impact. The water used in water ring vacuum pumps can become contaminated with process gases or chemicals, and may require treatment before disposal.
- Operating costs. Water ring vacuum pumps typically require a constant supply of water and may also require water treatment equipment, such as separators or condensers, to maintain proper operation. This can result in higher operating costs compared to other types of vacuum pumps.
Only registered users can write reviews
Related products

1 HP (0.81 kW) Water Ring Vacuum Pump
ATO-WRVP-01
$1,718.09
High quality and reasonable price water vacuum pump for sale online. Water ring vacuum pump with 1 hp power and 50 Hz frequency. The waterproof level of the water ring pump motor has reached IP54. 1 hp water ring type vacuum pump often used in chemical industry, electrical power system and pharmaceutical industry.

15 HP (11 kW) Water Ring Vacuum Pump
ATO-WRVP-15
$4,838.09
Reasonable price 15 hp water ring vacuum pump with close coupled design and stainless steel material for sale. The unique design of the discharge port can protect the vacuum pump from the over-pressure. Water ring type vacuum pump often used in chemical industry and electrical power system.

20 HP (15 kW) Water Ring Vacuum Pump
ATO-WRVP-20
$7,159.05
Single stage 20 hp water ring vacuum pump adopts with stainless steel material. The close-coupled design of liquid ring vacuum pump is convenient to install and can save space. Frequency of liquid ring vacuum pump is 50 Hz. The unique design of the discharge port ensures the best efficient performance in the working range of the vacuum pump.

5.5 HP (4 kW) Water Ring Vacuum Pump
ATO-WRVP-055
$2,970.23
Water ring type vacuum pump with 5.5 hp power and stainless steel material in affordable price for sale. Rated voltage of 5.5 hp water ring pump is 380V. The unique design of the discharge port ensure the best efficient performance in the working range of the 5.5 hp vacuum pump.